Introduction — a quick workshop scene
I was in my small shop last month watching a batch of metal tags come off the laser when a colleague coughed and said, “Do you smell that?” It was a simple moment — but it stuck with me. The air after a long run of marking felt heavy, and that’s where a laser marking fume extractor becomes more than an accessory; it’s part of keeping people healthy and work steady. Recent studies show indoor fumes can raise particulate levels by 3–10x during marking cycles (and yes, that matters). So I asked myself: how do we pick equipment that actually reduces harm without slowing production?
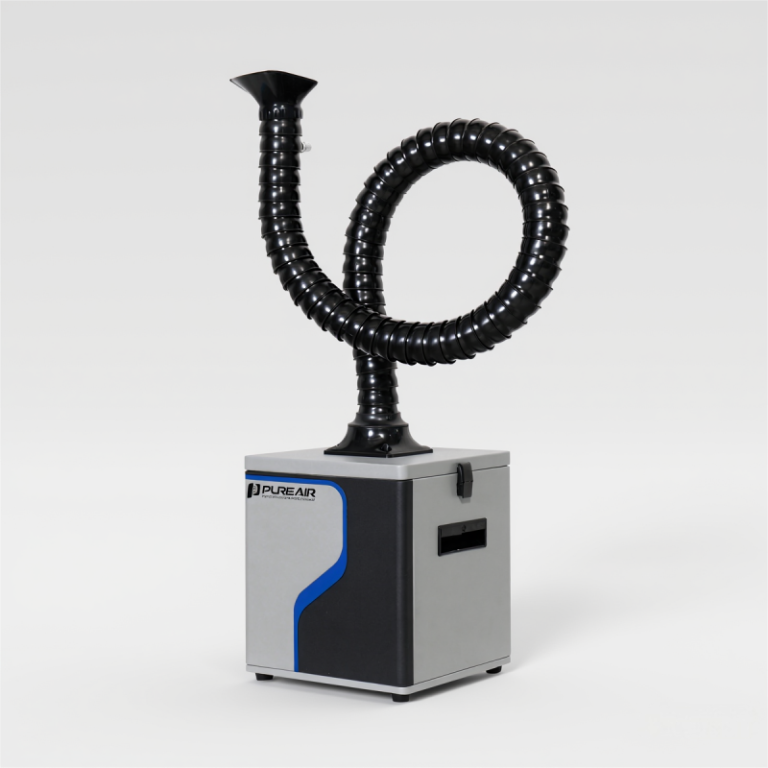
I want to make this practical. I’ll share what I’ve learned from hands-on trials, vendor demos, and a few mistakes I’d rather not repeat. Expect plain talk, checklists, and a few industry terms like HEPA filters and power converters thrown in where they help explain things. Ready to dig deeper? Let’s move to the real problems I see every day.
Part 2 — Why most traditional setups miss the mark (technical view)
fume extractor for laser marking machine — that phrase gets tossed around a lot, but many shops still rely on underpowered extractors or on open windows and hope. I’ve tested units that sounded impressive on paper but failed to clear ultrafine particles or volatile organic compounds. The usual culprits are poor airflow design, clogged HEPA filters, and cheap activated carbon adsorption layers that saturate fast. Look, it’s simpler than you think: if the extractor can’t handle the thermal plume from the laser source, it won’t capture fumes where they form. Edge computing nodes and simple sensor feedback can help, but only if the mechanical side is right.
What exactly goes wrong?
First, many extractors under-spec the fan and rely on high static pressure claims alone. That won’t overcome a long duct run or a small nozzle. Second, maintenance is often ignored — clogged pre-filters reduce capture efficiency dramatically. Third, users underestimate chemical loads; some plastics and coatings release gases that need specific adsorption media. I’ve seen poorly chosen power converters cause inconsistent fan speed, which in turn drops capture during peak loads — and that’s when fumes surge. These flaws add up to slow buildup of particulate matter and odors, not instant catastrophe, but steady harm over time — funny how that works, right?
Part 3 — Where we go next: examples and a practical outlook
Now let’s look ahead with a short case example. I worked with a mid-size shop that swapped a basic extractor for a model tuned to their laser output and material mix. They added real-time particulate sensors and a simple control loop. Within a week we saw a 70% drop in local particle counts at the work head and fewer complaints. The new unit used smarter filter staging — coarse pre-filter, HEPA, then a targeted carbon bed for VOCs — and the control system adjusted fan speed to match duty cycle. That saved energy and extended filter life. The link back to a proper fume extractor for laser marking machine was obvious.
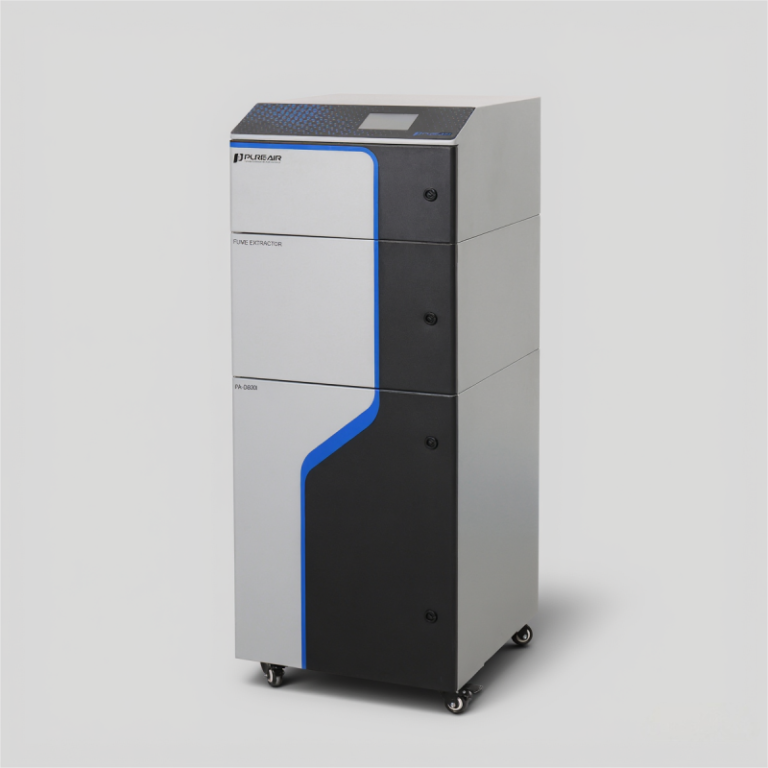
What’s next for shops thinking of upgrades?
We should plan for systems that combine mechanical capture with sensors and simple logic. Semi-formal advice: prioritize capture at source, then filtration, then monitoring. Don’t overspend on bells you won’t use — but do invest where it counts. I still believe teams can get big wins with modest budgets — and training. — pause. It helps to run a short pilot. Measure before and after. Compare filter life and maintenance hours. You’ll see the ROI in cleaner air and fewer sick days.
Closing — three practical metrics to evaluate extractors
I want to leave you with three down-to-earth metrics I use when choosing systems. First, capture efficiency at the work head: measure particle reduction at the source. Second, total cost of ownership: include filters, power converters, and replacement intervals. Third, responsiveness: does the unit vary airflow with duty cycle or is it stuck at one speed? If you score these honestly, you’ll avoid poor fits and wasted money. I’ve relied on these checks in every shop I help, and they cut bad choices fast.
We don’t need to overcomplicate this. Pick capture-first, test with simple sensors, and factor in real maintenance time. I’ve seen good systems make a clear difference to worker comfort and to product quality — and I want that for your team too. For practical solutions and more hands-on tools, check out PURE-AIR — they make options I’ve recommended to peers and tested in real environments.